Reducing Downtime in Freeze Drying: Long-Term Reliability of Maglev Vacuum Pumps in Pharmaceutical Manufacturing
Release time: Oct.22.2026
Click volume: Views
Pharmaceutical freeze drying, or lyophilization, is a critical stabilization technique used for thermolabile drugs, vaccines, biologics, and injectable formulations. The process requires extended cycles—often lasting days—under ultra-low temperatures and deep vacuum environments to sublimate ice directly from frozen products into vapor. Throughout this demanding cycle, vacuum pumps must operate continuously without failure to maintain chamber pressure integrity.
Traditional oil-sealed rotary vane or mechanical booster pumps are prone to mechanical wear, seal degradation, and oil contamination risks. In a pharmaceutical cleanroom, unscheduled downtime or lubricant backstreaming can ruin multi-million-dollar batch productions and trigger lengthy validation delays. To eliminate maintenance bottlenecks and secure 24/7 process reliability, pharmaceutical manufacturers are upgrading their freeze-drying vacuum systems to active magnetic levitation (maglev) oil-free vacuum pumps.
1. Vacuum Dynamics and Reliability Challenges in Lyophilization
The lyophilization cycle progresses through primary and secondary drying stages, where the vacuum system must evacuate large volumes of water vapor while pulling chambers down to deep ultimate pressures.
+-----------------------------------------------------------------------+
|             PHARMACEUTICAL FREEZE DRYING VACUUM ARCHITECTURE          |
|                                                                       |
|   [ Lyophilizer Drying Chamber ] ──> [ Condenser / Vapor Trap ]       |
|                                                  │                    |
|                                                  ▼                    |
|   [ Cleanroom Control System ] ────> [ Maglev Oil-Free Vacuum Pump ]  |
|                                                  │                    |
|                                                  ▼                    |
|   [ Exhaust Vapor Condenser ] ─────> [ Sterilization / Clean Exhaust ]  |
+-----------------------------------------------------------------------+
Core Operational & Maintenance Bottlenecks
High Risk of Lubricant Backstreaming: Oil-sealed pumps can introduce hydrocarbon vapors into vacuum lines during sudden power interruptions or seal wear, contaminating sterile drug products.
Vapor Tolerance and Corrosion: Sublimated moisture and aggressive cleaning agents (such as Vaporized Hydrogen Peroxide used in CIP/SIP cycles) degrade internal pump components, leading to frequent overhauls.
Unscheduled Production Downtime: Mechanical friction in traditional bearings and rotary vanes requires regular maintenance interventions, interrupting manufacturing schedules and driving up operational costs.
2. Why Maglev Vacuum Pumps Transform Pharmaceutical Freeze Drying
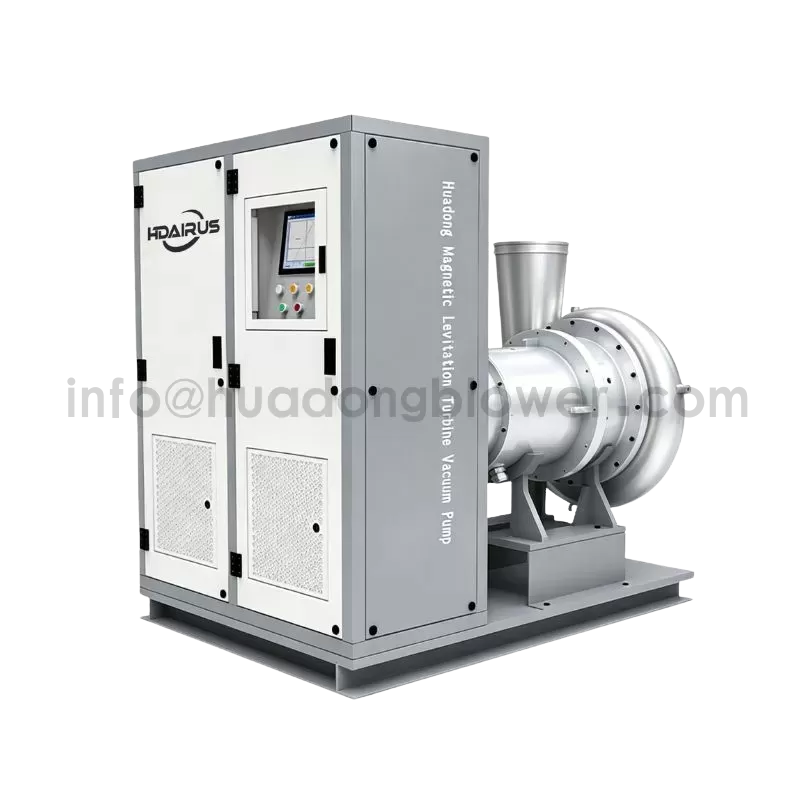
Maglev vacuum pumps integrate active magnetic bearings (AMB), permanent magnet synchronous motors (PMSM), and frictionless high-speed pumping technology, delivering unmatched operational reliability:
100% Oil-Free Cleanroom Purity: Magnetic levitation operates entirely without liquid lubricants or contact seals in the vacuum stream, completely eliminating oil backstreaming risks and ensuring regulatory compliance.
Frictionless Design for Maximum Uptime: With zero mechanical contact or bearing wear, maglev pumps eliminate the primary cause of pump failure, extending maintenance intervals and slashing unplanned downtime.
Precise Vacuum Control: High-speed digital controllers adjust pumping speeds dynamically, maintaining stable chamber pressure throughout delicate primary and secondary drying phases.
Reduced Total Cost of Ownership (TCO): Eliminating oil changes, filter replacements, and frequent mechanical overhauls significantly reduces maintenance labor and replacement parts expenditures.
3. Strategic Integration in Lyophilization Facilities
Freeze Drying Stage | Role of Maglev Vacuum Systems | Reliability & Quality Benefit |
Initial Chamber Evacuation | Rapidly pulls down system pressure to initiate primary freezing and sublimation thresholds. | Cuts batch preparation time and stabilizes initial chamber vacuum. |
Primary & Secondary Drying | Continuously evacuates sublimated water vapor under deep vacuum conditions. | Prevents product melt-back and ensures consistent residual moisture levels. |
Clean-in-Place (CIP) / Sterilization | Withstands rigorous cleanroom sterilization protocols without internal degradation. | Maintains sterility and supports rapid batch-to-batch turnaround. |
4. Manufacturing Standards by Shandong Huadong Blower Co., Ltd.
Shandong Huadong Blower Co., Ltd. is a premier manufacturer of advanced industrial fluid machinery and precision vacuum solutions. Operating from its 100,000 square meter smart manufacturing center in Zhangqiu, Jinan, China, the company engineers high-efficiency HDAirus maglev vacuum pumps and oil-free systems designed specifically to support critical pharmaceutical manufacturing and cleanroom applications.
Engineering Highlights of HDAirus Maglev Vacuum Systems
Advanced Active Magnetic Bearings: Real-time digital sensors maintain precise rotor levitation under varying thermal and vacuum loads, ensuring vibration-free operation.
Turnkey Cleanroom Integration: Factory-tested skid packages equipped with smart PLC controls, sanitary fittings, and clean exhaust management for seamless facility deployment.
By deploying HDAirus oil-free maglev vacuum technology into pharmaceutical freeze-drying lines, manufacturers eliminate downtime risks, protect product purity, and achieve long-term operational excellence.
Recommended Products