High-Vacuum Distillation Made Simple: Lowering Energy Consumption with Maglev Vacuum Pumps in Chemical Refining
Release time: Nov.05.2026
Click volume: Views
In chemical refining and petrochemical manufacturing, high-vacuum distillation is an essential separation technology used to purify heat-sensitive compounds, heavy hydrocarbons, specialty chemicals, and pharmaceutical intermediates. Operating distillation columns under deep vacuum lowers the boiling points of complex liquid mixtures, preventing thermal cracking, product degradation, and unwanted side reactions.
To achieve and sustain stable absolute vacuum pressures across massive columns, refineries traditionally rely on multi-stage steam jet ejectors, liquid ring vacuum pumps, or oil-sealed mechanical boosters. However, these legacy vacuum technologies carry severe drawbacks: steam ejectors consume massive quantities of boiler energy and generate contaminated wastewater condensate, while liquid ring and oil-sealed pumps suffer from high power draw, solvent contamination, and frequent seal maintenance. By upgrading to magnetic levitation (maglev) oil-free vacuum pumps, chemical refiners simplify system architecture, drastically lower energy consumption, and ensure unbroken process reliability.
1. Vacuum Dynamics and Energy Constraints in Chemical Distillation
High-vacuum distillation columns operate under deep vacuum conditions (often from 1 mbar down to sub-millibar levels) to enable low-temperature thermal separation.
+-----------------------------------------------------------------------+
|             CHEMICAL REFINING HIGH-VACUUM DISTILLATION LOOP           |
|                                                                       |
|   [ Distillation Column Overhead Vapor ] ──> [ Primary Condenser ]     |
|                                                     │                 |
|                                                     ▼                 |
|   [ Liquid Distillate Receiver ] ──────────> [ Reflux / Product Tank ]|
|                                                     │                 |
|                                                     ▼                 |
|   [ Smart DCS Control Panel ] ─────────────> [ Maglev Vacuum Pump ]   |
|                                                     │                 |
|                                                     ▼                 |
|   [ Solvent Recovery / Clean Exhaust ] ────> [ Emission Control Loop ]|
+-----------------------------------------------------------------------+
Core Operational Bottlenecks in Refinery Vacuum Systems
High Energy Consumption: Steam jet ejectors waste substantial boiler steam capacity, while liquid ring pumps consume excessive electrical energy to overcome fluid drag.
Contaminated Effluent & Wastewater Streams: Steam ejectors condense process vapors into steam condensate, creating large volumes of hazardous wastewater that require costly effluent treatment.
Process Vapor Contamination: Vacuum pump sealing fluids or lubricants mix with evacuated chemical solvent vapors, degrading sealing oil, clogging internal clearances, and requiring constant lubricant disposal.
2. Why Maglev Vacuum Pumps Transform Chemical Distillation
Maglev vacuum pumps combine active magnetic bearings (AMB), permanent magnet synchronous motors (PMSM), and frictionless high-speed molecular centrifugal mechanics, delivering clear operational advantages over legacy ejectors and liquid ring pumps:
Up to 40%–50% Energy Savings: Eliminating steam utility consumption and fluid drag resistance drastically reduces overall utility energy draw, yielding rapid return on investment (ROI).
100% Oil-Free & Contactless Operation: Magnetic levitation operates completely without liquid lubricants, sealing water, or contact seals in the vacuum path, guaranteeing zero process contamination and zero hazardous wastewater generation.
Deep & Stable Absolute Vacuum: Ultra-high-speed digital rotor control maintains precise, pulse-free vacuum levels across changing vapor loads, ensuring consistent column separation efficiency.
High Resistance to Corrosive Chemical Vapors: Specialized internal flow coatings and non-contact rotor clearances easily handle aggressive organic vapors and condensable solvents without mechanical wear.
3. Case Study: Specialty Chemical Refinery Upgrade
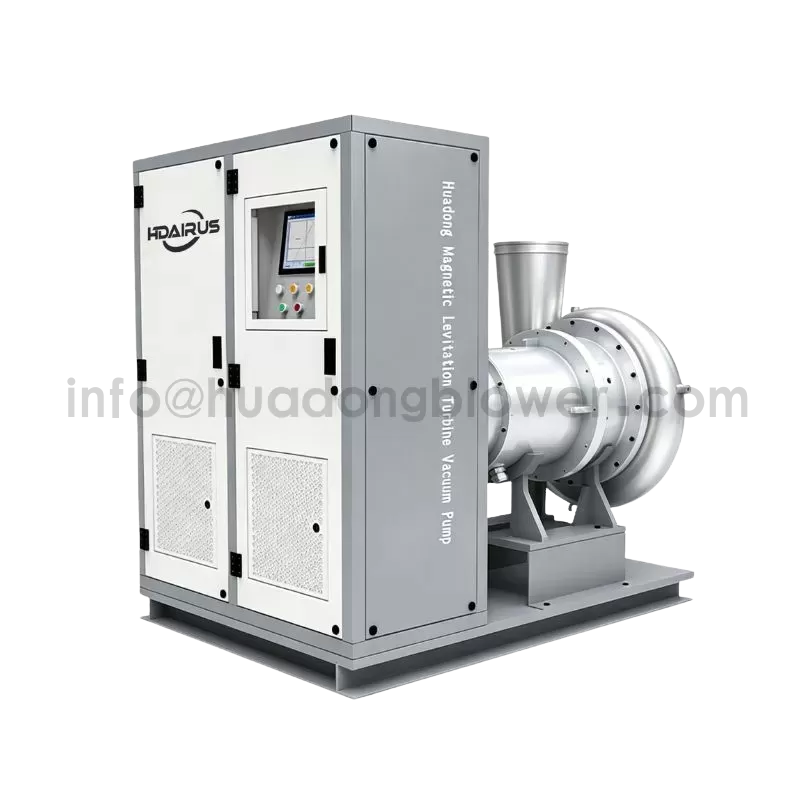
A specialty chemical plant processing high-boiling-point ester compounds retrofitted its vacuum distillation column by replacing a steam jet ejector and liquid ring combination with an HDAirus maglev oil-free vacuum skid package.
Implementation & Operating Parameters
Process Application: High-vacuum fractionating column for heat-sensitive ester purification.
Operating Vacuum Level: Sustained 2.0 mbar absolute pressure.
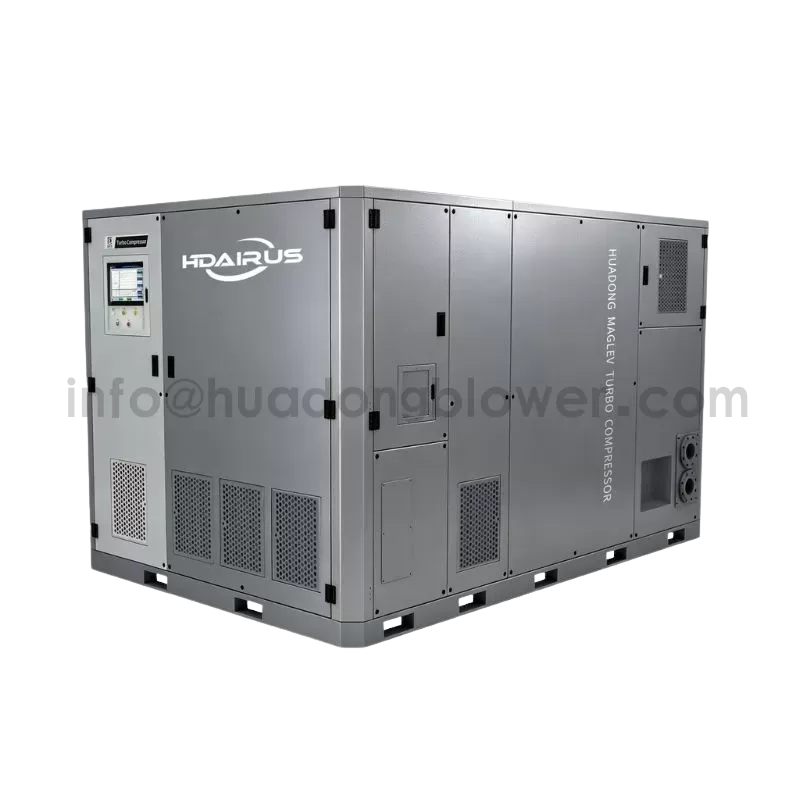
Equipment Integration: HDAirus maglev vacuum pump skid with integrated solvent recovery condenser and DCS communication interface.
Performance Optimization Metrics
Energy Overhead Reduction: Eliminated 1.2 tons/hour of low-pressure steam demand, reducing system energy consumption by 43%.
Wastewater Elimination: Completely eliminated hazardous steam condensate generation, saving significant wastewater treatment fees annually.
Product Yield Improvement: Sustained deep vacuum stability prevented thermal degradation, increasing high-purity product yield by 3.8%.
4. Manufacturing Capabilities of Shandong Huadong Blower Co., Ltd.
Shandong Huadong Blower Co., Ltd. is a premier manufacturer of advanced industrial fluid machinery and precision vacuum equipment. Operating from its 100,000 square meter smart manufacturing center in Zhangqiu, Jinan, China, the company engineers high-efficiency HDAirus maglev vacuum pumps and oil-free process air systems designed to support continuous, energy-efficient chemical refining worldwide.
Engineering Highlights of HDAirus Maglev Vacuum Systems
Precision Active Magnetic Bearings: Real-time digital sensors adjust rotor position thousands of times per second, maintaining contact-free levitation under dynamic vacuum loads.
Chemical-Grade Anti-Corrosion Protection: Advanced surface coatings protect internal flow channels and impellers against aggressive chemical vapors and condensates.
Turnkey Skid Package Architecture: Shipped as fully assembled, factory-tested vacuum skids equipped with integrated trap condensers, smart PLC touchscreens, and industrial DCS/SCADA interfaces.
By deploying HDAirus oil-free maglev vacuum technology into high-vacuum distillation loops, chemical refiners simplify operations, eliminate hazardous wastewater, and achieve maximum energy efficiency.
Recommended Products